View Factor Orientation (or View factor or shape factor) plays an important role in radiation heat transfer. View factor is defined as, "fraction of radiation leaving surface 'i' and strike 'j' ". Summation Rule (View Factor) If there is are similar surfaces 'i' and 'j' , then: Blackbody Radiation Exchange Radiation Exchange between Opaque, Diffuse, Gray surfaces in an Enclosure 1. Opaque 2. Surfaces 3. Two surface enclosure Radiation Shield It is used to protect surfaces from radiation act like a reflective surface. References: Material from Class Lectures + Book named Fundamentals of Heat and Mass Transfer by Theodore L. Bergman + My knowledge. Photoshoped pics are developed. Some pics and GIF from Google. Videos from YouTube ( Engineering Sights ).
Get link
Facebook
X
Pinterest
Email
Other Apps
Phases and Heat Treatment
Get link
Facebook
X
Pinterest
Email
Other Apps
-
Components
These are pure metals. Combination of components is called Alloy.
System ↠ refers to specific body (region) of material under consideration.
It is defined as, "Maximum concentration of solute atoms that may dissolve in solvent to form solid solution at specific temperature".
It depends on temperature.
Phases
It is defined as, "a homogenous portion of a system that has uniform physical and chemical characteristics".
Single-phase system ↠ homogenous system.
Two or more phase system ↠ heterogenous system.
Microstructure
It is defined as, "a subject to direct microscopic observation using optical or electron microscopes".
Microstructure is characterized by number of phases present, their proportion and manner in which they are arranged.
Microstructure of alloy depends on alloying elements, concentrations, heat treatment (temperature, heating time at temperature, rate of cooling to room temperature)
Phase Equilibria
It is defined as, "a system in which more than one phase may exist (consistency w.r.t time)".
Equilibrium is best described in a quantity called Free Energy.
A change in temperature, pressure, composition for a system result in increase in free energy.
Phase Equilibrium Diagram
It is defined as, "Information about the control of phase structure of a particular system is displayed".
Microstructures may develop from phase transformation (altered due to temperature change, cooling).
Common phase diagrams ↠ temperature and composition are variable (pressure = constant).
Binary phase diagrams ↠ represents relation between temperature, composition and quantities of phase.
Binary Amorphous System ↠ There are 3 types of phases
∝-Solution ↠ contains both material in solid form.
L-Solution ↠ contains both material in liquid form.
∝ + L Solution ↠ contains both phase.
Liquidous line ↠ above which phase is liquid and below it is mixture.
Solidous line ↠ below which phase is solid and above it is mixture.
Interpretation of Phase Diagram
For a binary system of known composition and temperature at equilibrium, we use 3 kind of information
Phases that are present ↠ point is above or below the solidous or liquidous line.
Composition of these phases ↠ Draw a tie line (horizontal line through point which lie in mixture area), Note intersection of tie line and the phase boundaries, Drop perpendicular from these intersections and note values.
Percentages or Fractions of phases ↠ Relative amount (as fraction or percentage) of phases present at equilibrium may be calculated using phase diagram.
Lever Rule
Tie line is constructed across two-phase region at temperature of alloy.
Overall alloy composition is located on tie line.
The fraction of one phase is computed by taking length of tie line from overall alloy composition to phase boundary for the other phase and dividing by the total tie line length.
The fraction of other phase is determined in the same manner.
The metal iron is a primary constituent of some most important engineering alloys.
Ingot Iron ↠ iron in its purest form.
Iron is an allotropic metal (exist in more than one lattice type depending upon temperature).
Phase changes of iron (info for cooling of pure iron):
Iron at 2800 F (solidification) ↠ BCC or δ-Form.
Iron at 2554 F (cooling) ↠ FCC or γ-Form and Non-magnetic.
Iron at 1666 F ↠ BCC or ⋉-Form and Non-magnetic.
Iron at 1414 F ↠ ⋉-Iron becomes magnetic without change in lattice structure.
Temperature at which allotropic changes take place ↠ depends on alloying elements.
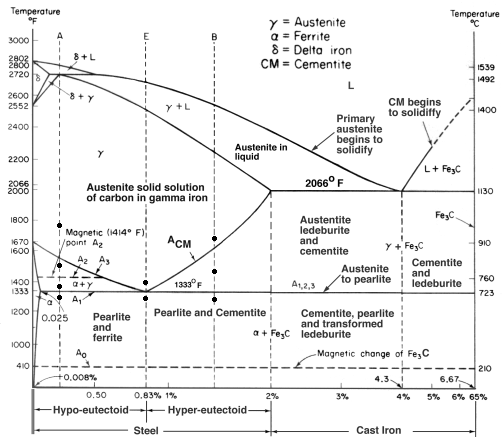
Diagram between pure iron and iron carbide (interstitial compound) Fe3C containing 6.67 % carbon by weight, so called Iron-Iron Carbide Equilibrium Diagram.
If have 0.8 % or less carbon in steel ↠ Hypo-eutectoid Steel.
If have (0.8-2) % carbon in steel ↠ Hyper-eutectoid Steel.
Hypo-eutectic Steel ↠ < 4.3 % carbon in steel.
Hyper-eutectic Steel ↠ (4.3-6.67) % carbon in steel.
Ques: Solubility of carbon in Austenite > that that in Ferrite?
Austenite has FCC crystal arrangement and packly closed together (i.e. high APF) than Ferrite.
Formation (or Growth) of Pearlite
Carbon in Austenite precipitate to form cementite (i.e. FCC → BCC). Carbon deposit on cementite boundary to form ferrite.
Classification of Steel
1. Method of Manufacture
This gives rise to Bessemer steel, Open-Hearth steel, Electric-Furnace steel, Crucible steel, etc.
2. Chemical Composition
By means of numbering system, indicate approx. content of important elements in steel.
Steps are as follows:
First digit of 4 or 5 numeral designation indicate type of steel used ( 1 → carbon steel, 2 → Nickel steel, 3 → Nickel-Chromium steel).
If simply alloy steel, 2nd digit indicates approx. percentage of predominant alloying element.
The last 2 or 3 digits usually indicate mean carbon content divided by 100.
Sometime steels are classified by broad range of carbon content:
Low-carbon Steel → up to 0.25 % carbon.
Medium-carbon Steel → 0.25 % - 0.55 % carbon.
High-carbon Steel → above 0.55 % carbon.
Heat Treatment of Steel
"A combination of heating and cooling operations, timed and applied to a metal or alloy in solid state in a way that will produce desired properties".
Heat treatment processes for steel involve transformation or decomposition of Austenite.
Nature and appearance of these transformation products determine the physical and mechanical properties of any given steel.
Steps for heat treatment of steel are:
Heat material to temperature above critical range to form Austenite.
Rate of heating to desired temperature is less important than other factors in heat-treatment cycle.
Highly stressed material (by cold work) → heat more slowly than stress free to avoid distortion.
Difference in temperature rise within thick or thin sections of variable cross-section should be considered → heat slow thinner sections to minimize thermal stress and distortion.
A. Full Annealing or Furnace Cooling
It is defined as, "process consists of heating steel to proper temperature and then cooling slowly through transformation range (in furnace)".
Purpose → refine grains, induce softness, improve electrical and magnetic properties, improve machinability.
Reason → Annealing is a very slow cooling process → close to follow Iron-Iron Carbide Equilibrium diagram (because of entire mass of furnace is cooled with material).
For Hypo-Eutectoid steel → rise temperature from A1 to A3 to get fine grain structure → than furnace cooling to get fine grain of Ferrite and Pearlite.
For Hyper-Eutectoid steel → use temperature above A3,1 but have poor machinability.
Microscopic study of proportions of ferrite and pearlite or pearlite and cementite present in an annealed steel enable us to determine approx. carbon content of steel.
B. Spheroidizing
It is defined as, "annealing process to improve the machinability".
Because annealed hyper-eutectoid steel with a microstructure of pearlite and cementite → gives poor machinability.
Steps:
Prolong holding at a temperature just below the lower critical line.
Heating and cooling between temperature that are just above and below the lower critical line.
Heating to a temperature above the lower critical line and then cooling very slowly in the furnace or holding at a temperature just below the lower critical line.
Stress-Relief Annealing
It is defined as, "process used to remove residual stresses due to heavy machining or other cold working processes".
Carried out below critical line (1000-1200 F)
Process Annealing
"It is similar to stress-relief annealing in sheet and wire industries carried out by heating the steel to a temperature below the lower critical line (1000-1200 F)".
Applied after cold working and soften the steel by recrystallization.
C. Normalizing
It is defined as, "process carried out by heating approximately 100F above the upper critical temperature (A3 or ACM) line followed by cooling in still air to room temperature".
Purpose → to produce harder and stronger steel than full annealing.
Final heat treatment operation.
Cooling rate is high due to air cooling as compared with furnace cooling affects the transformation of austenite.
It is defined as, "the strength and hardness of some metal alloys may be enhanced by the formation of extremely small, uniformly dispersed particles of a second phase within the original phase matrix induced by heat treatment".
Precipitate → small particles of the new-phase.
Age Hardening → because strength of material develops with time.
Types of Heat Treating
Steps are:
An appreciable max. solubility of one component in the other.
A solubility limit that rapidly decreases in concentration of the major component with temperature reduction.
a. Solution Heat Treating
It is defined as, "All solute atoms are dissolved to form a single-phase solid solution".
Consist of heating the alloy to a temperature within the ∝-phase (To) and waiting untill all the β-phase that may have been present is completely dissolved.
b. Precipitation Heat Treating
It is defined as, "The supersaturated ∝-solid solution is heated to an intermediate temperature T2 within ∝+β (or 2-) phase region at which diffusion rates become appreciable".
Aging → β-phase form fine dispersed particles of composition Cβ.
Overaging → strength or hardness increases with time and reaches a max. value, after that strength (and hardness) reduces after long time.
β-Particles Character → (i.e. strength and hardness) depend on precipitation temperature T2 and aging time.
Solid Mechanics OR Mechanics of Materials OR Strength of Materials: It is the study of mechanics of body i.e. forces and their effects on deformable solids under different loading conditions. Deformable Body Mechanics: It is the study of non-rigid solid structures which deform under load. Deformation/Distortion ⇾ change of shape and size OR have some relative displacement or rotation of particles. It happens when we apply combined load. Rigid Body Motion ⇾ Translation or rotation of particles but having constant distance between particles. Since deformation occur at particular load. Below this load, every body is considered as rigid body . Types of Load: Point Load ⇾ Load apply on a single point i.e. concentrated load. Uniformly Distributed Load (UDL) ⇾ Load remains uniform throughout an area of element like beam. Varying Distributed Load (VDL) ⇾ Load varies with length with constant rate. Moment ⇾ It measures the tend...
Mechanical Injection System: Used to inject fuel into the combustion chamber. Fuel speed > air speed at delivery point to atomize fuel. Amount of fuel delivered into the air stream going into the engine is controlled by pump which forces the fuel under pressure. A device used to initiate and control the combustion process is called Mechanical Injection System. Functional Requirements of Injection System: Metering of Fuel: Used to control fuel to meet speed and load requirements of the engine. Injection Timing: Have proper injection timing to obtain max. power, fuel economy and proper burning. It is done by Camshaft or Push rod (Rocker Arm) Mechanism . Proper Control of Injection Rate: To get desired heat release pattern during combustion. Proper Atomization of Fuel: Proper making of droplets to make best Air/Fuel mixture. Proper Spray Pattern: Distribution of droplets to ensure rapid mixing of fuel & air. Uniform Distribut...
Flexible Mechanical Elements Flexible mechanical elements are defined as, " I nelastic elements to transmit power over large distances " . Purpose of using FME's is to simplify the design of a machine and reduce the cost . Used as replacement for gears, shafts, bearings, other rigid power-transmission devices. It can absorb shock loads and vibrations. Positive Drive ⇛ no slip between driver and driven component. Element Life ⇛ no infinite life and should be replaced at the first sign of deterioration (check wear, aging, loss of electricity). Performance of Different Transmission Types Belts or Belt Drives Belts are used where center distance between shafts is large. Pulley axes must be separated by a certain minimum distance (depend upon belt type and size) to operate properly. Because of belt flexibility and damping capability ⇛ reduce the transmission of unwanted shock and vibration between shafts. Power and torque capacities are limi...




Comments
Post a Comment
HI, we wI'll contact you later