View Factor Orientation (or View factor or shape factor) plays an important role in radiation heat transfer. View factor is defined as, "fraction of radiation leaving surface 'i' and strike 'j' ". Summation Rule (View Factor) If there is are similar surfaces 'i' and 'j' , then: Blackbody Radiation Exchange Radiation Exchange between Opaque, Diffuse, Gray surfaces in an Enclosure 1. Opaque 2. Surfaces 3. Two surface enclosure Radiation Shield It is used to protect surfaces from radiation act like a reflective surface. References: Material from Class Lectures + Book named Fundamentals of Heat and Mass Transfer by Theodore L. Bergman + My knowledge. Photoshoped pics are developed. Some pics and GIF from Google. Videos from YouTube ( Engineering Sights ).
Get link
Facebook
X
Pinterest
Email
Other Apps
Bulk Forming Processes
Get link
Facebook
X
Pinterest
Email
Other Apps
-
Bulk Forming Processes:
Bulk refers to workparts with low surface area to volume ratio.
Bulk Forming uses heavy machine to apply three dimensional stresses.
There are 4 basic operations used for bulk deformation:
Rolling
Forging
Extrusion
Wire & Bar Drawing
1. Rolling:
Deformation process in which work thickness is reduced by compressive forces exerted by two opposite rolls.
Variations in rolling are described ahead:
A. Types of Rolling Based on Workpiece Geometry:
I. Flat Rolling:
It is used to reduce thickness of a rectangular cross-section.
II. Shape Rolling:
It is used to deform workpiece into contoured cross-section.
B. Types of Rolling Based on Work Temperature:
I. Hot Rolling:
The material is heated to a uniform elevated temperature to achieve significant deformation.
Parts are free from residual stresses.
II. Cold Rolling:
Hot materials (like plates or sheets) are further flatten by cold rolling to prepare them for metal operations at room temperature.
It further strengthen material.
C. Thread Rolling:
It us a cold rolling process used to form threads on cylindrical parts by rolling them between two dies.
D. Ring Rolling:
It is used to reduce the wall thickness and increase the diameter of a ring.
E. Gear Rolling:
It is a cold working process used to produce gears.
2. Forging:
Manufacturing processes that induce plastic deformation through localized compressive forces applied through two opposing dies.
Varations in forging are:
A. Types of Forging Based on Work Temperature:
I. Hot or Warm Forging:
Deformation is done at high temperatures but it reduces strength and increases ductility of work metal.
II. Cold Forging:
It increases the strength of material results from strain hardening of work metal.
B. Types of Forging Based on Shape of Dies:
There different types of forging but we dicuss some of them:
I. Open-Die Drop-Hammer Forging:
The metal is heated to a specific temperature by furnace or electrical indunction then work is compressed between two flat dies.
Only for large objects or for small number of parts.
If no friction between work and die surfaces then homogeneous deformation.
The opposition to flow of work metal due to friction between die and work is called Barreling Effect.
Open die drop hammer forging are further classifies as:
Fullering ⇔ performed to reduce the cross-section by dies with convex surfaces.
Edging ⇔ performed to reduce the cross-section by dies with concave surfaces.
Cogging ⇔ used to reduce cross-section and increse length. Also called Incremental Forging.
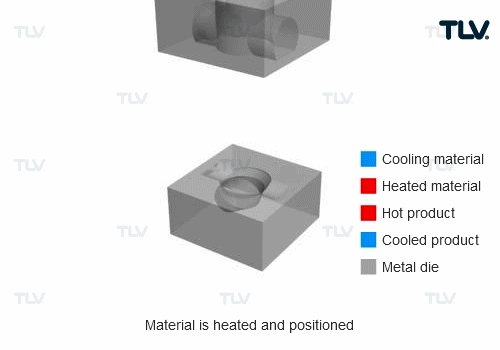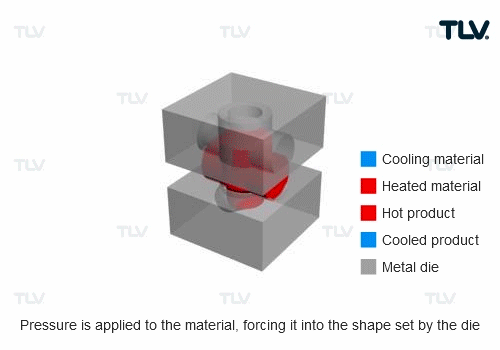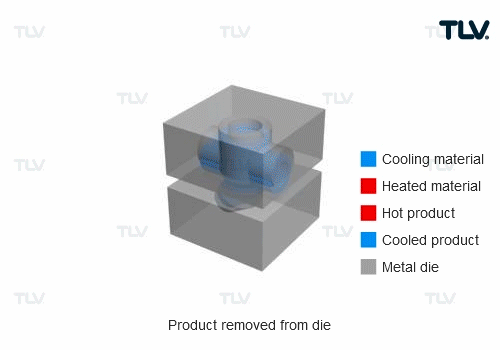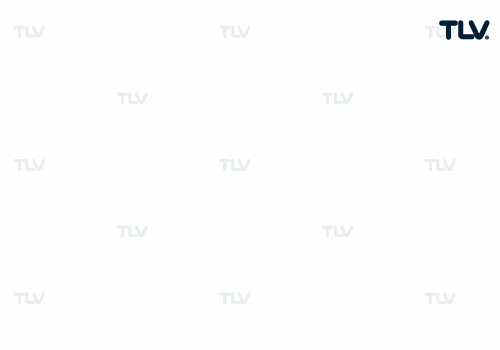
II. Impression-Die Drop-Hammer Forging:
The work peice is deformed between two die halves which carry impressions of Desired final shape.
III. Swaging (or Rotary Swaging or Radial Forging):
It uses rotating dies which hammer the work peice to reduce the diameter to create a tapered section.
3. Extrusion:
Compression forming process in which the work metal is forced to flow through a die opening to produce a desired cross-sectional shape.
There are two types of extrusions:
A. Direct Extrusion (or Forward or Hot or Continuous Extrusion):
A hot working process in which final material move in the same direction as that of the force applied is called Direct Extrusion.
Significant friction is present between work and die surfaces.
Length of final material is not limited.
B. Indirect Extrusion (or Backward or Reverse or Cold or Discrete Extrusion):
A cold working process in which final material move in the direction opposite to that of force applied is called Indirect Extrusion.
Frictional effects are not that significant as used to be in Direct Extrusion.
Length of material is limited.
4. Wire & Bar Drawing:
Wire Drawing is defined as:
It us used to reduce the diameter of wire having stock diameter less than 9mm.
Bar Drawing is defined as:
It is used to reduce the diameter of bars or rod having stock diameter greater than 9mm.
Reference:
University Notes
Book Fundamental of Modern Manufacturing 6th Edition by Mikell P. Groover
Mechanical Injection System: Used to inject fuel into the combustion chamber. Fuel speed > air speed at delivery point to atomize fuel. Amount of fuel delivered into the air stream going into the engine is controlled by pump which forces the fuel under pressure. A device used to initiate and control the combustion process is called Mechanical Injection System. Functional Requirements of Injection System: Metering of Fuel: Used to control fuel to meet speed and load requirements of the engine. Injection Timing: Have proper injection timing to obtain max. power, fuel economy and proper burning. It is done by Camshaft or Push rod (Rocker Arm) Mechanism . Proper Control of Injection Rate: To get desired heat release pattern during combustion. Proper Atomization of Fuel: Proper making of droplets to make best Air/Fuel mixture. Proper Spray Pattern: Distribution of droplets to ensure rapid mixing of fuel & air. Uniform Distribut...
Solid Mechanics OR Mechanics of Materials OR Strength of Materials: It is the study of mechanics of body i.e. forces and their effects on deformable solids under different loading conditions. Deformable Body Mechanics: It is the study of non-rigid solid structures which deform under load. Deformation/Distortion ⇾ change of shape and size OR have some relative displacement or rotation of particles. It happens when we apply combined load. Rigid Body Motion ⇾ Translation or rotation of particles but having constant distance between particles. Since deformation occur at particular load. Below this load, every body is considered as rigid body . Types of Load: Point Load ⇾ Load apply on a single point i.e. concentrated load. Uniformly Distributed Load (UDL) ⇾ Load remains uniform throughout an area of element like beam. Varying Distributed Load (VDL) ⇾ Load varies with length with constant rate. Moment ⇾ It measures the tend...
ENGINEERING SURVEY Surveying is the science, art and technology of determine the relative positions of points above, on or beneath the Earth's surface so as to construct a map, plan or description. TYPES OF SURVEY : There are many types of survey but we discuss some of them. 1. Plane & Geodatic Survey : Ordinary field and topographical surveying in which the Curvature of Earth's surface is disregarded is called Plane Survey. It is performed when the area is smaller than 250sq.km. A survey of a large land area in which corrections are made for the Curvature of Earth's surface is called Geodatic survey. Why Geodatic Survey is important? Earth's surface is not flat, it is sphere. So all the calculations which were made by considering the Earth's surface flat are incorrect. So a new type of survey came into play which made calculations on the basis of geodatic condition of Earth's surface. 2. Topographic Survey : Topographic surv...




Comments
Post a Comment
HI, we wI'll contact you later