View Factor Orientation (or View factor or shape factor) plays an important role in radiation heat transfer. View factor is defined as, "fraction of radiation leaving surface 'i' and strike 'j' ". Summation Rule (View Factor) If there is are similar surfaces 'i' and 'j' , then: Blackbody Radiation Exchange Radiation Exchange between Opaque, Diffuse, Gray surfaces in an Enclosure 1. Opaque 2. Surfaces 3. Two surface enclosure Radiation Shield It is used to protect surfaces from radiation act like a reflective surface. References: Material from Class Lectures + Book named Fundamentals of Heat and Mass Transfer by Theodore L. Bergman + My knowledge. Photoshoped pics are developed. Some pics and GIF from Google. Videos from YouTube ( Engineering Sights ).
Get link
Facebook
X
Pinterest
Email
Other Apps
Advance High Strength Steel (AHSS)
Get link
Facebook
X
Pinterest
Email
Other Apps
-
Advance High Strength Steel
Conventional low carbon mild steel has simpler ferritic structure (α-iron) and good ductility.
Common type of HSS is High Strength Low Alloy (HSLA) ⇥ has yield strength 550 - 690 N/sq.mm.
Manganese ⇥ supporter (stabilizer) of ferrite.
Conventional HSS:
Is single-phase ferritic steel with a potential for some pearlite in C-Mn steel.
Lower strain hardening capacity.
Advance HSS:
primarily steel with a microstructure containing a phase other than ferrite, pearlite, cementite.
Crumple Zone ⇥ Made with those materials which absorb maximum amount of energy.
Safety Cage ⇥ Multiple areas (like cabins, structural elements).
Areas of Safety cage are described ahead:
Cabins (Blue Areas) ⇥ Should have high strength with a good balance of strength, formability, energy absorption and durability.
Structural Elements (Red Areas) ⇥ Safety critical parts.
Conclusion is:
Dual phase (DP) & Transformation induced plasticity (TRIP) steels are excellent in crash zone (high energy absorption capacity), so it is used to make Crumple Zone.
For structural elements ⇥ Extremely high strength steels such as Martensite and Boron-based Press Hardened (PHS) steels are used.
Advance HSS Family
Dual Phase (DP)
Complex Phase (CP)
Ferritic Bainitic (FB)
Martensite
Transformation Induced Plasticity (TRIP)
Hot Formed (HF)
Twinning Induced Plasticity (TWIP)
Dual Phase (DP) Steel
It consist of a ferritic matrix containing a hard martensite second phase in the form of island.
Microstructure is produced by giving steel a Sub-Critical Anneal at 800℃ and is quenched to room temperature.
Sub-Critical Anneal ⇥ Heating a material (steel) lower than the equilibrium line between austenite and α-phase and then cool it.
Ferrite is unaffected by heat treatment but Austenite grains transformed to martensite during quenching and is tempered at low temperature to increase ductility.
Tempering ⇥ heat treatment process that is performed in steels containing martensite just to relief some stresses.
DP Steel exhibits high work hardening rate, ultimate tensile strength, Tensile & Yield strength ratio.
Transformation Induced Plasticity (TRIP) Steel
It consist of Austenite embedded in a primary matrix of ferrite.
To get retained austenite ⇥ use Step Quenching (from Transformation Time VS Transformation Temperature Graph)
TRIP steel has lower initial work hardening rate than DP.
It uses higher quantities of carbon than DP to obtain sufficient carbon content for stabilizing the retained austenite phase to below ambient temperature.
Si & Al ⇥ used to avoid carbide precipitation in the bainite region.
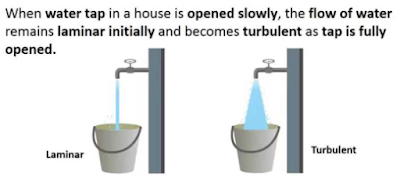
Reynolds Number: Reynolds Number is the ratio of Inertial forces to the Viscous forces. By knowing this number, one can describe the flow whether the flow is laminar, turbulent or transitional flow. There are three possibilities of the range of Reynolds Number: If Reynolds number < 2100 or 2300 ⟺ Laminar Flow If Reynolds number > 4000 ⟺ Turbulent Flow If 2300 < Reynolds number < 4000 ⟺ Transitional Flow In case of different shapes other than circle, the formula for Reynolds Number remain the same however diameter involves in the formula become Hydraulic Diameter which is given by: For pipe: Critical Reynolds Number ⟾ The Reynolds number at which the flow becomes turbulent Re cr For different shapes, the hydraulic diameters are given by: Completely Filled Flow In Closed Channel: If pipe is is considered to filled completely with closed channel, then following are the conditions which...
Gear Forming by Machining Formation of gear through machining consists of following methods: Form Milling by Disc Cutter Form Milling by End Mill Cutter Shaper, Planner and Slotter Broaching 1. Form Milling by Disc Cutter It is defined as, " Tooth is cut one by one by plunging the rotating cutter into the blank " . Each gear needs a separate cutter. 8 - 10 standard cutters are available for producing 12 - 120 teeth gears. Used for big spur gears of large pitch. 2. Form Milling by End Mill Cutter It includes the cutting of tooth at a time and then indexed for the next tooth space for cutting. For a small volume production of low precision gears. Set of 10 cutters ↠ 12 - 120 teeth gears . Used for teeth of large gears/module. To reduce cost, same cutter is often used for multiple sized gears resulting in profile errors . Characteristics: Use of Hardened stainless steels (HSS) form milling cutters. Use of Ordinary milling machines. Low production rate (need of indexing...
Mechanical Injection System: Used to inject fuel into the combustion chamber. Fuel speed > air speed at delivery point to atomize fuel. Amount of fuel delivered into the air stream going into the engine is controlled by pump which forces the fuel under pressure. A device used to initiate and control the combustion process is called Mechanical Injection System. Functional Requirements of Injection System: Metering of Fuel: Used to control fuel to meet speed and load requirements of the engine. Injection Timing: Have proper injection timing to obtain max. power, fuel economy and proper burning. It is done by Camshaft or Push rod (Rocker Arm) Mechanism . Proper Control of Injection Rate: To get desired heat release pattern during combustion. Proper Atomization of Fuel: Proper making of droplets to make best Air/Fuel mixture. Proper Spray Pattern: Distribution of droplets to ensure rapid mixing of fuel & air. Uniform Distribut...




Comments
Post a Comment
HI, we wI'll contact you later