View Factor Orientation (or View factor or shape factor) plays an important role in radiation heat transfer. View factor is defined as, "fraction of radiation leaving surface 'i' and strike 'j' ". Summation Rule (View Factor) If there is are similar surfaces 'i' and 'j' , then: Blackbody Radiation Exchange Radiation Exchange between Opaque, Diffuse, Gray surfaces in an Enclosure 1. Opaque 2. Surfaces 3. Two surface enclosure Radiation Shield It is used to protect surfaces from radiation act like a reflective surface. References: Material from Class Lectures + Book named Fundamentals of Heat and Mass Transfer by Theodore L. Bergman + My knowledge. Photoshoped pics are developed. Some pics and GIF from Google. Videos from YouTube ( Engineering Sights ).
Get link
Facebook
X
Pinterest
Email
Other Apps
Entropy
Get link
Facebook
X
Pinterest
Email
Other Apps
-
Entropy:
It is defined as;
Measure of irreversibilities or randomness of the system.
Clausius Inequality:
The clausius inequality is developed from the Kelvin-Planck statement of the 2nd Law and can be expressed as:
The inequality of clausius is a consequence of the 2nd Law of thermodynamics.
Where;
Q is the heat transfer to or from the system.
T is the absolute temperature at the boundary.
The symbol ∮ is the cyclic integral.
For total reversible and for internally Reversible:
A special case of Internally Reversible Isothermal Heat Transfer Process:
In Isothermal Process, temperature doesn't change (so it is treated as constant)
Entropy change will be positive or negative when:
For heat transfered ↝ Entropy is positive
For heat rejected ↝ Entropy is negative
Increase of Entropy Principle:
The total Entropy is given by:
Now, for the the process 1 to 2 and 2 to 1 is given by:
Entropy Change of a Pure Substance:
The Entropy change for pure substance is given by:
ΔS = m Δs
ΔS = m ( s2 - s1 )
Isentropic Process:
Entropy of a fixed mass can be changed by two ways:
By Heat transfer
By Irreversibilities
It means that for an adiabatic internally reversible process, the Entropy will not change. Such a process is called Isentropic Process.
Q. A Reversible adiabatic process is always Isentropic but an Isentropic process doesn't mean that the process is adiabaticlly reversible. Explain?
If heat change is negative that is heat is given out but the losses always increase Entropy and if they are equal with opposite sign , so total Entropy is zero.
Q. What is the area under the internally reversible process curve on a T-S diagram indicate?
Now the differential area is equal to the product of temperature and differential Entropy.
Mollier Diagram:
Diagram between enthalpy and Entropy ( h-s ) is called Mollier Diagram.
T ds Relation:
The differential form of conservation of energy equation for closed stationary system containing a simple compressible substance can be expressed for an internally reversible process as:
This equation is called 1st TdS equation or Gibb's Equation.
Furthermore;
The above equations (3) and (4) are important as they relate the entropic changes in terms of changes in their properties.
Entropy changes of Solids and Liquids:
Since there is no effect of pressure on liquids and solids so there is no change in volume.
dV ⋍ 0
Cp = Cv = C
So, equation (3) becomes:
Entropy Change of Gases:
For Gases:
1. Using Constant Specific Heat method:
2. Using Variable Specific Heat method:
When the temperature change during a process is larger, then the constant specific heat assumption cannot be used. For this purpose, we define new function S° called reference Entropy.
Isentropic Process of Ideal Gases:
1. By using Constant Specific Heat method:
2. Using Variable Specific Heat method:
Steady Flow Reversible Work:
Energy balance for a steady flow devices undergoing an internally reversible process can be expressed in a differential form as:
If,
d k.e. ⋍ 0
d p.e. ⋍ 0
So above equation becomes:
Q. Why steam is superheated before sending it to the turbine?
Since, reversible steady flow work is proportional to the specific volume, therefore superheating is done to kept specific volume as high as possible so as work output.
Q. Why cooling is done during compression?
Since, reversible steady flow work is proportional to the specific volume, therefore cooling is done to kept specific volume as low as possible so as work input.
Q. What is the area to the left on an internally reversible process curve on a PV Diagram?
Now the differential area is equal to the product of Specific Volume and differential pressure.
Area to the left of process curve is steady flow reversible work.
Minimizing the Compressor Work:
It can be minimized by maintaining the temperature of the gas as low as possible by cooling during the compression process.
Isentropic compression ↝ Adiabatic therefore no cooling, high work input
Polytropic compression ↝ Moderate cooling
Isothermal compression ↝ maximum cooling, °•° least work input.
Thermal Efficiency:
When the Compressor is operated at Isothermal Process, it's work input is minimum, so the Isothermal efficiencies compares the actual work input to the Isothermal efficiencies compares the actual work input to the Isothermal compressor work input.
Q. Out of the above compression process which one will have least work input?
Since, area to the left of the process curve on a PV Diagram indicates steady flow reversible work. So, the Isothermal Process has the least area to the left of the curve and Isentropic has the maximum work.
Steady Flow Reversible Work for:
1. Isentropic Process:
As we know for an isentropic process:
Now, formula for work done:
From the very first equation:
2. Polytropic Process:
As we know for a Polytropic Process:
Now, formula for work done is:
3. Isothermal Process:
As we know for an Isothermal Process:
Now, formula for work done is:
Multi-stage Compression:
Multi stage compression is in between cooling by water or oil by water jack.
Now the formula for the input compressor work is given by:
The Px value that gives the minimum value if work input cab be found by differentiating Px. The above expression and setting the resultant expression equals to zero.
After simplifying:
Isentropic Efficiencies of Steady Flow Devices:
The isentropic efficiency is the measure of the derivation of actual processes from the corresponding idealized ones. In Isentropic efficiency, the ideal processes are Isentropic processes.
1. Isentropic Efficiency of Turbines:
Now the Isentropic efficiency is given by:
2. Isentropic Efficiency of Compressor:
Now the Isentropic efficiency is given by:
3. Isentropic Efficiency of Pump:
Now the Isentropic efficiency is given by:
4. Isentropic Efficiency of Nozzles:
Now the Isentropic efficiency is given by:
Note: If anyone wants me to publish a post on your topic related to mechanical engineering, Ielts, robotics, Web designing, etc, I am glad to see your interest and I can entertain you as well.
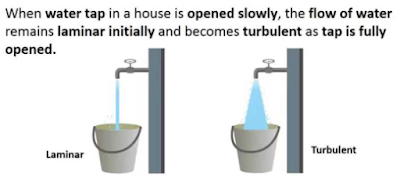
Reynolds Number: Reynolds Number is the ratio of Inertial forces to the Viscous forces. By knowing this number, one can describe the flow whether the flow is laminar, turbulent or transitional flow. There are three possibilities of the range of Reynolds Number: If Reynolds number < 2100 or 2300 ⟺ Laminar Flow If Reynolds number > 4000 ⟺ Turbulent Flow If 2300 < Reynolds number < 4000 ⟺ Transitional Flow In case of different shapes other than circle, the formula for Reynolds Number remain the same however diameter involves in the formula become Hydraulic Diameter which is given by: For pipe: Critical Reynolds Number ⟾ The Reynolds number at which the flow becomes turbulent Re cr For different shapes, the hydraulic diameters are given by: Completely Filled Flow In Closed Channel: If pipe is is considered to filled completely with closed channel, then following are the conditions which...
Intersection Of Solids: Solids are obtained by the combination of of two or more basic solids. When two or more solids combine, a definite curve/line is seen at their intersection. This curve/line is called curve/line of intersection (COI / LOI) and it is the result of inter-penetration of solids. Applications Of Intersection Of Solids: Designing a sheet metal objects. Automobile Parts. Moulding patterns. Forged end of connecting road. Intersection of two contacting surface, etc. Inter-Penetration Of Solids: When one solids penetrates another solids then their surfaces intersect and at the junction of intersection a typical curve is formed, which remains common to both solids. This curve is called Curve of Intersection and it is a result of inter-penetration of solids. Cases Of Intersection Of Solids: First we need to discuss the general solution steps of how we draw intersection of solids diagram. So know, we are going to discuss the basic steps:...
Types Of Lines And Its Uses: There are three types of types on the basis of thickness and they are: Visible Lines ↝ It represents features that can be seen in the current view. Hidden Lines ↝ It represents features that cannot be seen in the current view. Center Line ↝ It represents symmetry, path of motion, centers of circles,, axis of asymmetrical parts. Dimension and Extension Lines ↝ It indicates the sizes and location of features on a drawing. Placement Of Dimension Lines: Dimension should be outside the view. Dimension should be applied to one view. Dimension should be placed in a view that shows the distance in its true length. Dimension lines should be placed, in general 10 mm (1/2 in) away from the outlines from the view. Parallel lines should be placed uniformly. Values should be midway (auto centered) between the arrow heads, except when a center-line interferes. Dime...




Comments
Post a Comment
HI, we wI'll contact you later